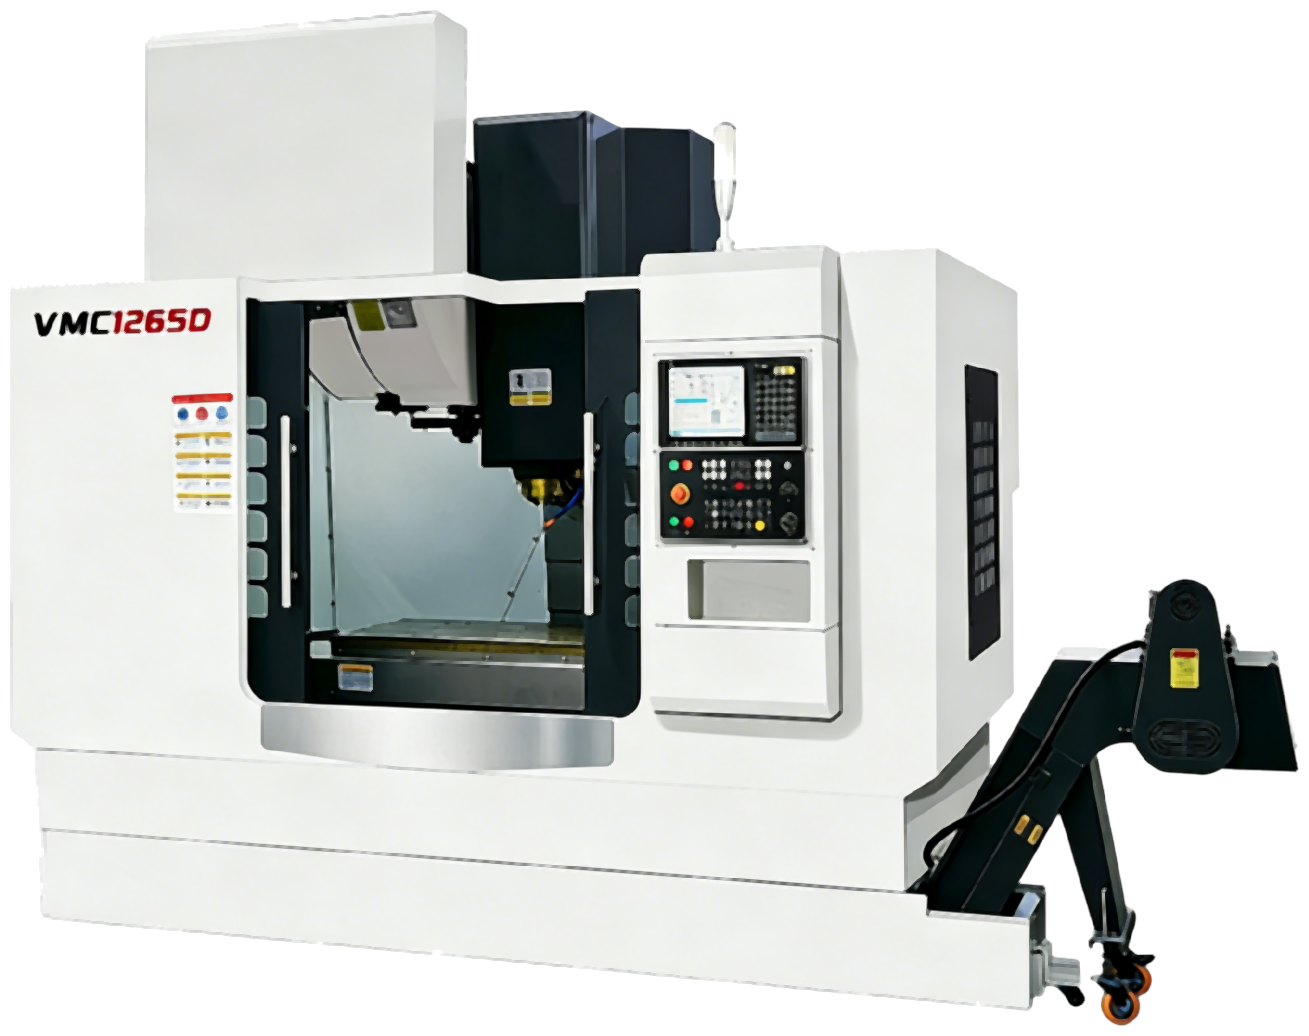
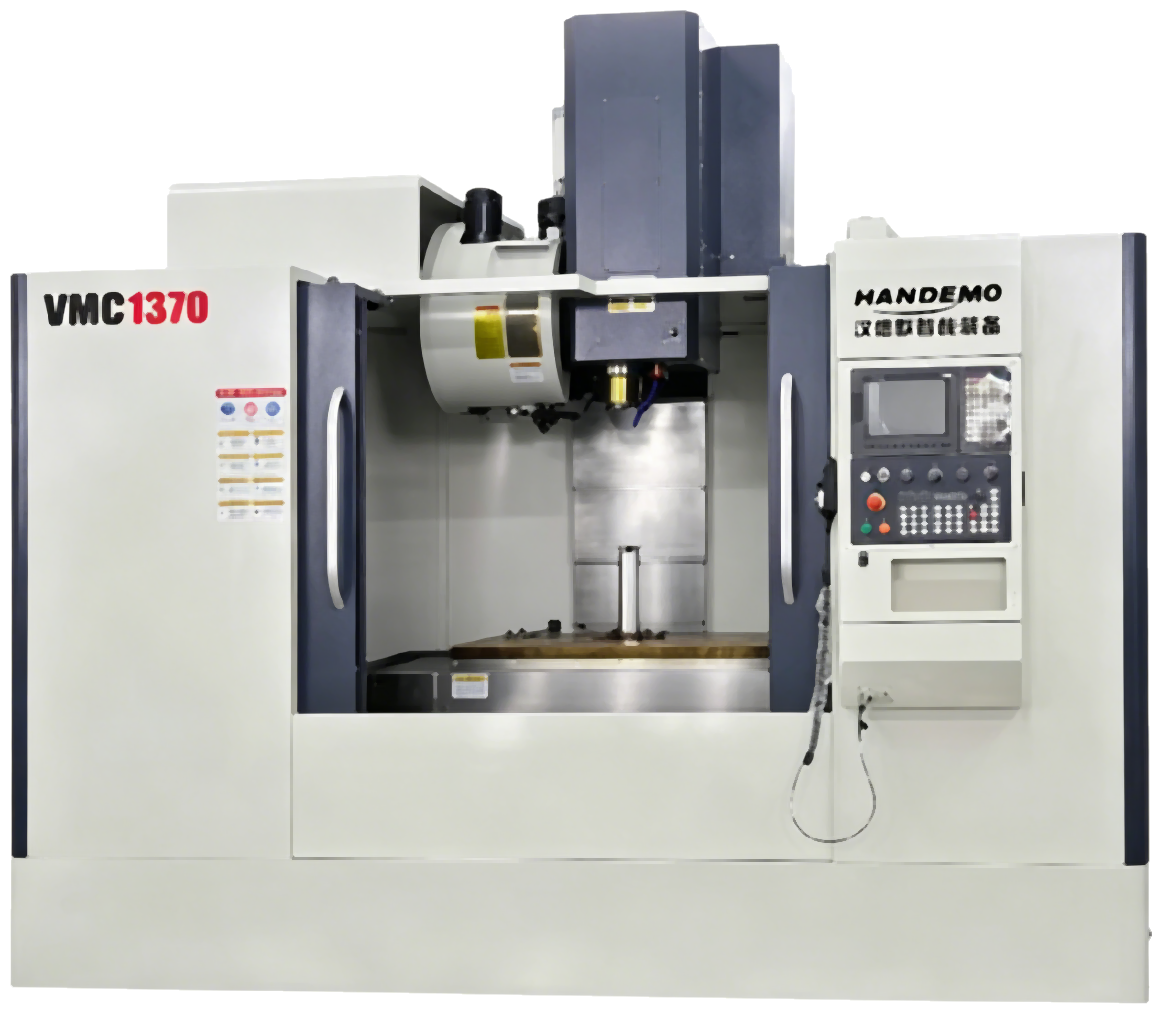
VMC1265D
VMC1265D
Discuss cavity work on a 1200 mm envelope.
1200×600 mm table1200 / 650 / 650BT40Φ150
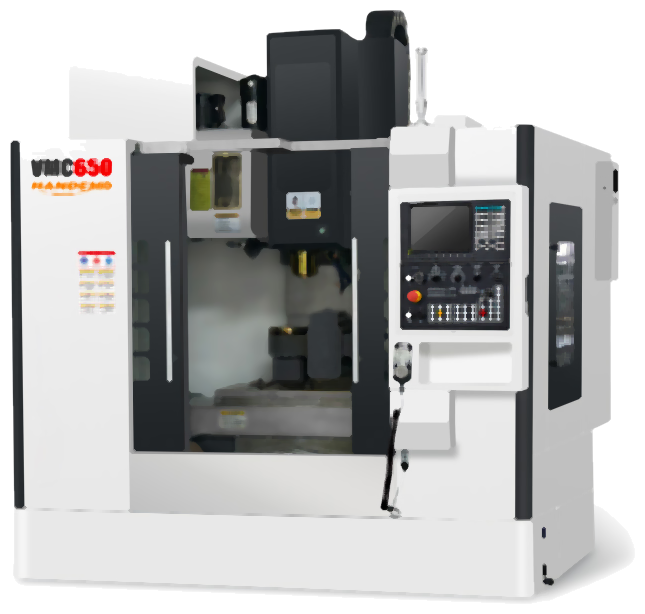
VMC866 · Mold & die VMC
For mold work at higher spindle speeds.
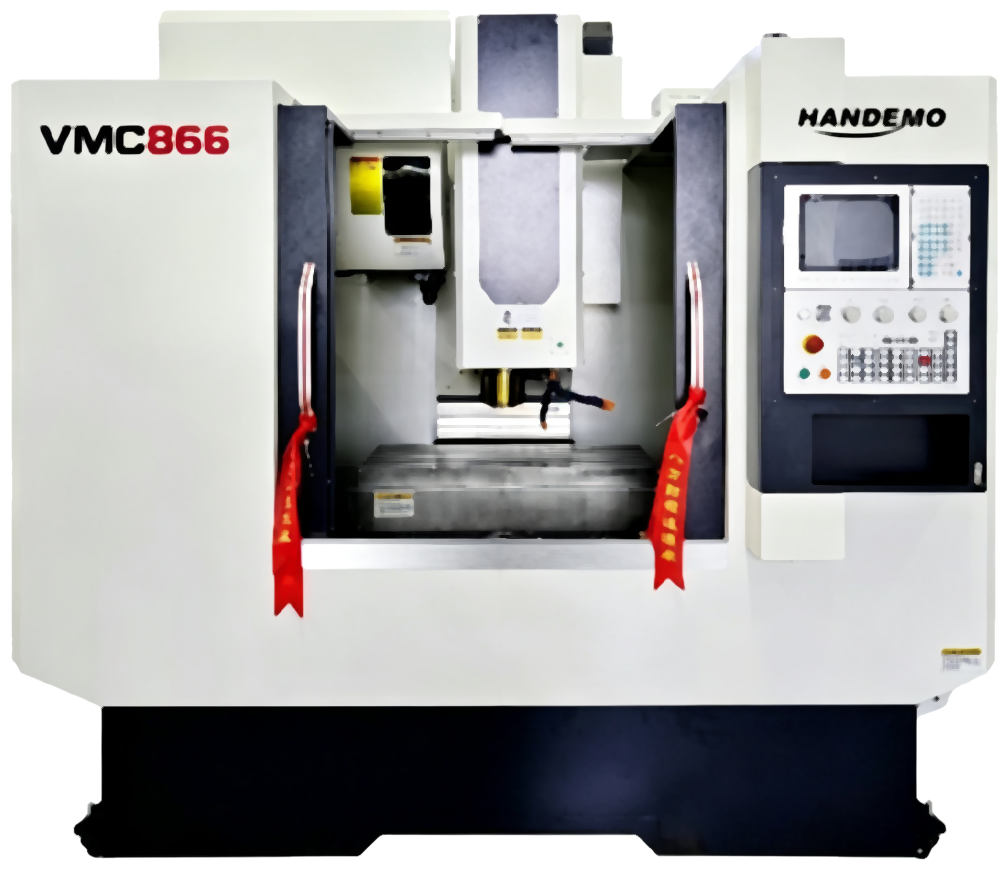
Machine details
The 855 platform set up for mould work: 1,000 x 550 mm table, 850 x 600 x 600 mm travels and a BT40 spindle at 8,000 rpm with 32 m/min rapids for long finishing passes.
Three linear guides on every axis, 45-size, with C3 ballscrews fixed at both ends. The higher rapid rate — 32 m/min in X and Y, 24 m/min in Z — matters on mould work, where most of the cycle is the tool following a surface rather than removing bulk. The spindle runs to 8,000 rpm on a BT40 taper with a 150 mm nose.
The table is 1,000 x 550 mm and carries 600 kg, enough for a mould base plus its clamping set. A 24-station disc magazine changes tools in 2.5 s. Positioning is 0.008 mm and repeatability 0.005 mm to JIS B6336-4 and GB/T 18400.4-2010. The machine stands 2,600 x 2,380 x 2,400 mm and weighs about 5,300 kg.
Typical applications are injection-mould inserts, die-cast tooling and electrode machining, where the requirement is surface finish and positional accuracy between the cavity and the water-line holes rather than metal removal rate. Options include 30/50/70 bar through-spindle coolant, a 12 L oil cooler, a 32-station magazine and an oil-mist collector.
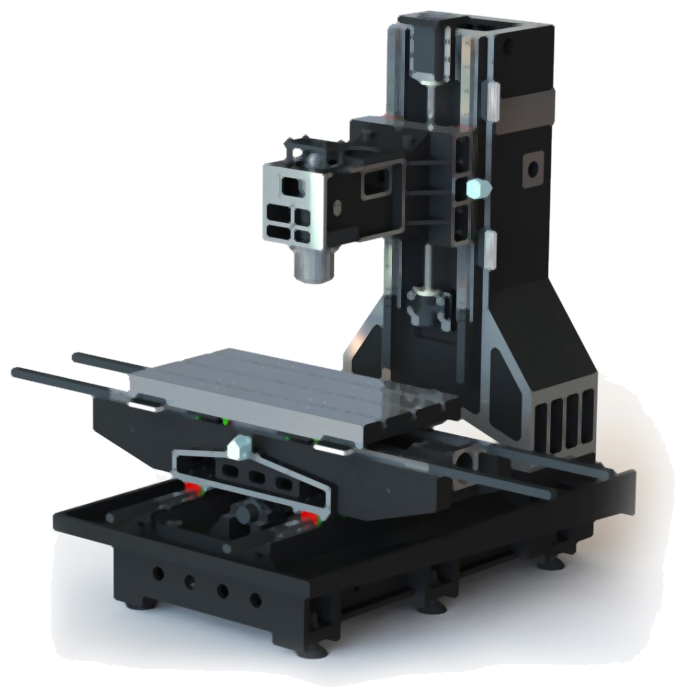
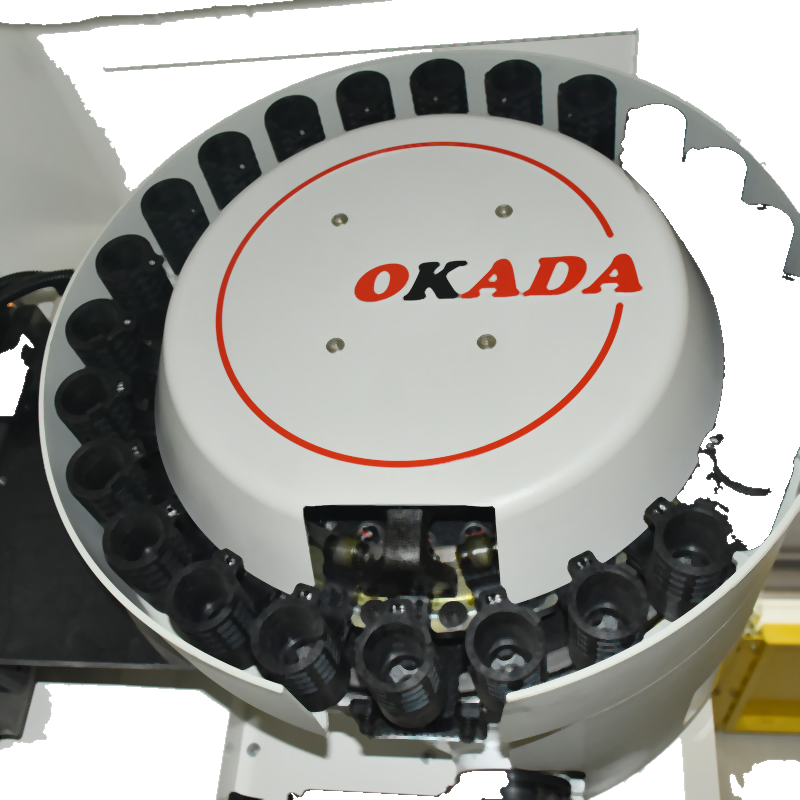
Detail photographs show the machine family and options. Final configuration is confirmed on the signed specification sheet.
Reference specifications
Missing values mean the item was not listed on the source sheet, not that the machine lacks the feature. Request the signed specification sheet for a full list.
Configuration
Material, blank size, features and tolerance.
Milling, drilling, tapping and fixturing.
Batch size, changeover and loading method.
Spindle, tooling, workholding and automation.
Molds and cores, plates and fixtures, housings, brackets and general prismatic parts. Application fit is confirmed against the part drawing.
Machine, standard tooling package, controller, documentation and commissioning scope as listed in the quotation.
Service & support
Drawing, material, tolerance and batch size.
Controller, spindle, tooling and workholding.
Foundation, utilities and agreed training scope.
Information, parts and service arrangements.
Same platform family
Discuss cavity work on a 1200 mm envelope.
Send the drawing, material and batch size. We will review the configuration with you.